Product catalogue
SPECTRA · DENTAL RESINS
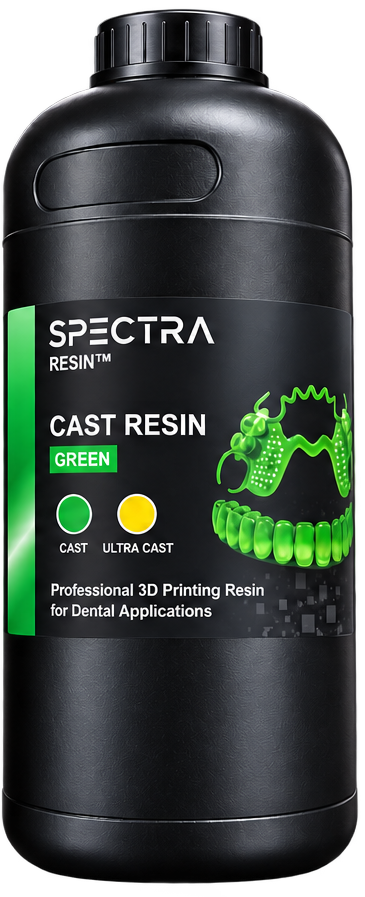
Cast & Ultra Cast resin
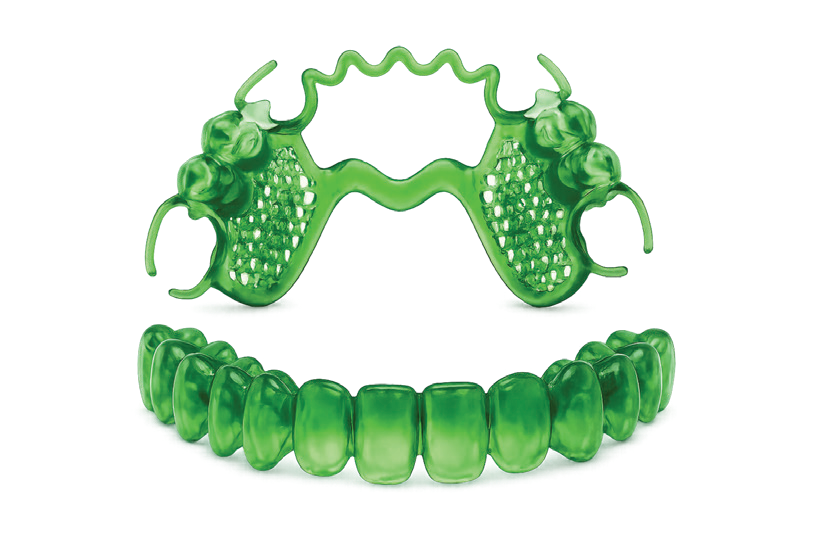
Sacrificial patterns for dental investment casting, followed by resin-compatible investment and controlled burnout.
Material highlights
- Digital pattern production
- Two clearly identified product options
- A dedicated casting workflow at the end of this catalogue
SPECTRA · SHADE GUIDE
Find your shade
Select a tooth to choose your pack and quantity.
Cast & Ultra Cast resin2 shades
Outlined teeth do not have a colour preview yet. You can still select them by name.
Colours are estimates from the supplied Spectra guide and may vary by screen. Confirm the final shade with a physical sample.
Colours and pack weights follow the catalogue; reference codes and availability are confirmed with the team.
Technical reference
The Cast match to the D-CAST reference profile must be confirmed. No dedicated Ultra Cast technical data or validated cycle is supplied; Cast values must not be transferred to it.
Mechanical properties
| Property | D-CAST |
|---|---|
| Flexural strength | 39.81 MPa |
| Flexural modulus | 811.08 MPa |
| Elongation at break | 8.85 % |
| Hardness | 85–88 Shore D |
Selected reported values. Results depend on formulation and specimen conditioning. Reported mechanical values carry a ±10% tolerance; hardness is presented as a range. Testing references: ASTM D638 (tensile), D790 (flexural) and D2240 (hardness).
Reference print settings & test conditions
Catalogue reference settings for matching materials, tested on ELEGOO MARS 3. Confirm resin variant and batch, and calibrate on the actual printer; these are not ready-to-use GK3 or universal printer presets.
| Property | D-CAST |
|---|---|
| Bottom exposure | 30–50 s |
| Normal exposure | 3–5 s |
| Layer height | 0.05 mm |
|---|---|
| Bottom/normal lift distance | 6 mm |
| Bottom lift speed | 60 mm/min |
| Normal lift | 80 mm/min |
| Retract speed | 150 mm/min |
| Rest after retract | 2–3 (unit not stated in source) |
| Test platform | ELEGOO MARS 3 |
| Test screen | 6.6-inch monochrome LCD |
| Irradiance | 3,500–4,500 µW/cm² |
Lift distance by screen size
| Below 7 inches | 6 mm |
|---|---|
| 7–10 inches | 8–10 mm |
| 10.1 inches | 11 mm |
| 13.3 inches | 14 mm |
| 15 inches | 15 mm |
These distances apply to the conventional release-film setup described in the source. Gingiva Mask calls for a 20–30% increase in lift distance. Validate against the actual machine and film. Bottom layer count = bottom thickness ÷ layer height + 1. For 0.40 mm at 0.05 mm per layer: 9 bottom layers. Mix resin thoroughly before printing. Run a calibration specimen whenever material, printer, light output, layer height or release film changes. Check detail, fit and separation before production.
Test specimen conditions
| Source test environment | 23 ± 2°C |
|---|---|
| Relative humidity | 50 ± 5% |
| Test specimen curing medium | water |
| Curing time per side | 1 min per side |
| Wavelength | 405 nm |
| Irradiance | 200 mW/cm² |
These are test-coupon conditions. They are not a validated clinical post-curing protocol for every SPECTRA resin.
Casting workflow & reference burnout cycle
The following pages summarise the supplied casting guide. Its cycle must be confirmed for the exact resin, investment, ring configuration and alloy. Ultra Cast has no separate validated cycle in the supplied files. Derived ramp rate: approximately 4.44°C/min. Confirm compatibility with the resin, investment and alloy; furnace performance and ring size may require a validated alternative cycle.
- Clean the pattern with the prescribed IPA process and dry it. Remove unnecessary supports and clean again. The casting guide limits optional post-curing to no more than 1 minute; confirm the exact resin instructions before applying this limit.
- Attach suitable wax sprues and centre the assembly. The supplied guide specifies clearance greater than 5 mm between the pattern and ring. Vacuum-mix a resin-compatible investment and pour carefully without directing the stream onto fine patterns.
- Investment selection, liquid/powder ratio and setting time must follow the investment instructions. Use an investment rated for the intended burnout temperature.
- The supplied guide illustrates centrifugal casting, followed by natural cooling, divesting and sandblasting. Select the alloy casting conditions, cooling sequence and finishing process according to the alloy and investment instructions.
| Entry temperature | 550°C |
|---|---|
| Ramp | 550 to 950°C over 90 minutes |
| Hold | 950°C for 30 minutes |
| Derived ramp rate | Approximately 4.44°C/min |
Washing & post-curing
Select the wash medium from the exact resin instructions; the reference distinguishes IPA-cleanable materials from water-washable model resin. Remove residual liquid, dry and inspect before curing. Final properties depend on wavelength, irradiance, time and part geometry; clinical applications require their validated protocol. Follow the safety data sheet and collect contaminated wash liquid for appropriate disposal.
SPECTRA · DOCUMENTS
Technical documents
Guides and catalogues for this product. Each file lists its document language.
Need another technical document for this product?
Request technical document